 Heavy Industry
Commutator .Supply DC Motor Commutator
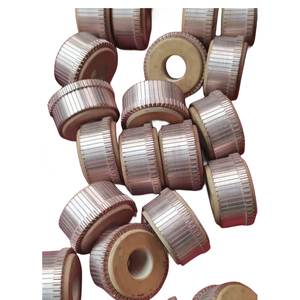
Heavy-duty industrial DC commutator featuring silver-bearing electrolytic copper segments designed for continuous high-torque operations in rolling mills and heavy machinery.
High-duty copper commutator rings engineered for optimal current reversal, minimal spark generation, and extended brush life across Austrian manufacturing plants.
Heavy Industry
Heavy-duty industrial DC commutator featuring silver-bearing electrolytic copper segments designed for continuous high-torque operations in rolling mills and heavy machinery.
 Precision 12-Segment
12-segment micro-switch dynamic commutator engineered with reinforced mica insulation for automated drive systems and precision Austrian industrial equipment.
 Universal Duty
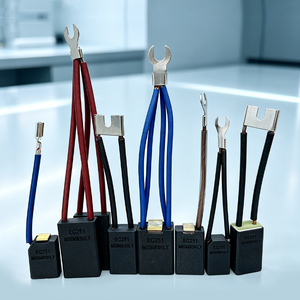
High-temperature universal brush collector assembly compatible with EG251 grade carbon brushes, providing smooth sliding contact and reduced commutator wear.
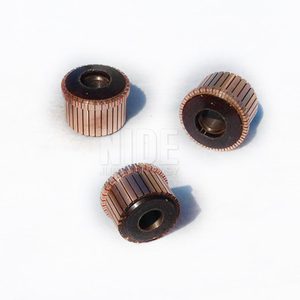 Traction Grade
V-ring arc-welded armature commutator ring optimized for high-vibration electric locomotive and cable car traction drive motors operating in Alpine terrain.
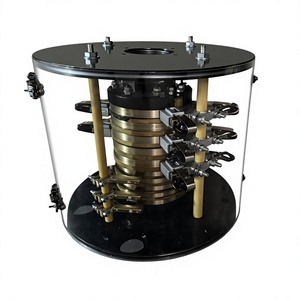 380V / 600V High Voltage
Heavy copper pack collector ring assembly featuring special-shaped bore mounting for continuous 360-degree rotating industrial machinery and cranes.
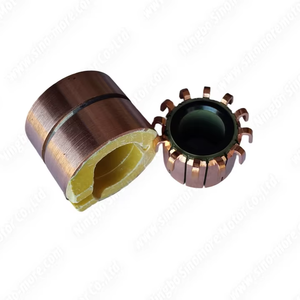 Hook-Type High Speed
Precision hook-type copper head collector ring designed for high-RPM generator armatures, power tools, and auxiliary motor assemblies.
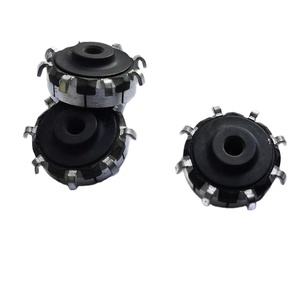 Automotive Grade
Compact automotive-spec DC motor commutator collector manufactured under zero-defect quality controls for severe weather wiper systems and auxiliary actuators.
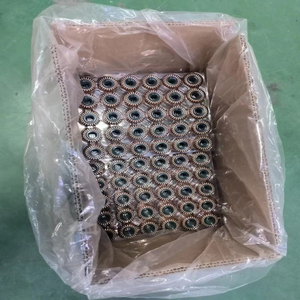 High Efficiency
Low-resistance copper alloy commutator ring configured for optimal current reversal, minimizing thermal losses in variable-speed industrial drives.
An authoritative technical analysis on commutator ring degradation, silver-bearing copper metallurgy, mica insulation dielectric stability, and ISO dynamic balancing for industrial plants in Austria.
Standard oxygen-free copper softens at operational temperatures exceeding 180°C, causing bar lifting and commutator eccentricity. Our factory utilizes high-purity CuAg0.1 (CW013A) silver-bearing copper containing 0.08% to 0.12% silver content. This alloy elevates the re-crystallization temperature beyond 340°C, maintaining micro-hardness (HV > 95) under extreme mechanical stress and thermal surges typical in Austrian steel production mills.
Inter-segment insulation breakdown leads to severe arc flashover and motor destruction. We employ premium rigid Muscovite and Phlogopite reconstituted mica bonded with alkyd-epoxy or silicone resins compliant with IEC 60371-3. Offering dielectric withstand strength exceeding 25 kV/mm, our segment separators resist thermal degradation up to Class C (180°C – 220°C+), insulating reliably against high inductive voltage spikes during current reversal.
Commutator integrity relies on precision clamping pressures. Our V-ring and shell-type commutator assemblies undergo high-temperature spin curing (baking cycles up to 200°C) combined with hydraulic press seasoning. This process locks copper segments and mica wedges into a rigid structural arch, eliminating "high bar" or "low bar" movement under high rotational forces up to 15,000 RPM.
The table below presents standardized technical parameters verified across our testing facilities in accordance with DIN 43021 and IEC 60034 standards for heavy industrial DC motor refurbishments.
| Parameter / Specification | Standard Grade Copper | Silver-Bearing CuAg0.1 (Our Standard) | Refractory Profile Option |
|---|---|---|---|
| Softening Temperature | 180°C - 200°C | 340°C - 370°C | 400°C+ |
| Electrical Conductivity | 100% IACS | 98.5% - 100% IACS | 95% IACS |
| Vickers Hardness (HV) | 80 - 90 HV | 95 - 115 HV | 120 - 140 HV |
| Max Dynamic Eccentricity | < 0.015 mm | < 0.003 mm (ISO G2.5) | < 0.002 mm |
| Insulation Resistance | > 50 MΩ | > 500 MΩ @ 2.5kV DC | > 1000 MΩ |
| Applicable Motor Types | Standard Fractional DC | Heavy Duty Industrial, Traction, Steel Mill | Military & Aerospace Actuators |
Custom engineered commutator rings tailored to the operational demands of Austria’s key manufacturing hubs—from Linz steel plants to Alpine transport networks.
Heavy industry operations such as cold rolling mills, hot strip mills, and continuous casting lines in Upper Austria demand DC drive motors capable of coping with intense shock loads and high torque reversals. Our silver-copper commutators resist severe thermal expansion cycles without mica displacement, preventing commutator segment lifting and costly unscheduled furnace shutdowns.
Mountain ropeway drive motors (Seilbahnantriebe) and funicular railways operate under stringent safety regulations governed by Austrian federal transport laws. Our traction-grade commutator rings undergo 100% ultrasonic flaw detection and spin-over-speed testing up to 150% rated RPM, guaranteeing flawless reliability in freezing temperatures and high-humidity mountain environments.
Austria’s electrified rail infrastructure relies on heavy-duty DC and AC traction motors. Our OEM direct-replacement armature commutators and collector assemblies strictly adhere to EN 60034-1 standards. Featuring TIG-welded armature riser slots, they prevent solder melting during steep gradient elevation pulls across the Arlberg and Semmering rail routes.
Hydroelectric power stations throughout Carinthia and Tyrol utilize large auxiliary motors and exciters. Our collector rings and commutator components provide corrosion-resistant, high-purity copper contact surfaces, mitigating carbon dust build-up and preventing flashovers in damp dam pump rooms.
Precision manufacturing plants producing automotive components and industrial automation require ultra-smooth commutator surfaces. We execute diamond-tool micro-turning on every commutator assembly, achieving bar-to-bar profile accuracy within 0.002 mm for quiet, spark-free brush operation.
Continuous paper machines require uniform speed control across multi-drive motor lines. Our dynamic commutator rings maintain consistent surface film formation, protecting carbon brushes against aggressive industrial chemical vapors present in pulp processing facilities.
Navigating EU Ecodesign directives, industrial remanufacturing initiatives, and green transition strategies within the DACH industrial sector.
In alignment with Austria’s "Kreislaufwirtschaftsstrategie" (Circular Economy Strategy), industrial plant managers are shifting from complete motor replacements to high-precision remanufacturing. Re-engineering worn DC armatures with high-grade replacement commutator rings reduces embodied carbon by up to 80% compared to new motor production, while restoring motor efficiency to original OEM specifications.
Energy loss in DC machines often stems from elevated contact voltage drops and electrical sparking across the brush-commutator interface. By utilizing sub-micron precision mica undercutting and V-groove chamfering on every bar edge, our factory-supplied commutators minimize electrical harmonics, reduce brush friction losses, and lower operating heat—contributing directly to plant energy optimization audits.
With European industrial supply chains focusing on nearshoring and inventory security, Austrian maintenance service companies cannot afford 12-week lead times from overseas. Our centralized European dispatch network ensures rapid transit of standard and custom commutator rings to Austrian industrial zones, backed by 24-hour technical support response guarantees.
Over 120 years of rotating machine excellence, backed by internationally recognized quality management systems and professional electrical trade memberships.
Founded at the dawn of industrial electrification, our engineering team possesses unmatched archival data and reverse-engineering capabilities for historic and modern DC motor frames, ensuring 100% dimensional accuracy for all replacement commutators.
Using unique motor serial number tracking systems, we store exact drawing specs, copper profiles, riser dimensions, and brush contact angles for thousands of industrial motors, streamlining replacement procurement without lengthy site measurements.
Every commutator ring undergoes rigorous quality checks: bar-to-bar insulation testing at 2,500V DC, high-speed spin testing at elevated temperatures, optical profile scanning, and dynamic balance certification according to ISO 1940 Grade G2.5.
Quality Management System
Electrical Apparatus Service Assoc.
Association of Electrical & Mechanical Trades
Answers to common technical queries regarding custom commutator manufacturing, material certifications, delivery logistics, and emergency maintenance support serving Austria.
Yes. We specialize in reverse-engineering legacy motor components. Whether you operate older BBC (Brown Boveri), Siemens, Schorch, or T-T Electric DC motors, our engineering team can rebuild or replicate exact replacement commutators from physical samples, worn shells, or technical drawings, matching original shaft tolerances and riser keyways perfectly.
For heavy-duty applications subject to thermal shock and high current density (e.g., steel rolling mills in Linz), we strongly recommend CuAg0.1 (Silver-Bearing Electrolytic Copper). The addition of 0.1% silver prevents annealing and softening under operating temperatures up to 340°C, maintaining segment tightness and preventing bar lifting under continuous load.
All industrial commutators are delivered with precision undercut mica depth (typically 0.8 mm to 1.2 mm depending on segment pitch) and 45-degree edge chamfering on every copper segment bar. This prevents mica whiskers from coming into contact with carbon brushes, eliminating flashovers and rapid brush friction wear.
Traction and high-speed commutators undergo a strict double-curing seasoning process followed by dynamic balancing to ISO 1940 Grade G2.5. They are tested in an overspeed spin chamber at elevated temperatures (150°C - 180°C) at speeds up to 1.5 times maximum operational RPM to guarantee zero bar movement prior to factory dispatch.
Every shipment includes complete EN 10204 Type 3.1 Material Test Reports verifying copper alloy chemistry and electrical conductivity (IACS), Dielectric Withstand Test Certificates (2.5kV DC bar-to-ground / bar-to-bar), Dynamic Balance Certificates, and CE compliance documentation.
Standard replacement commutator rings in our stock catalog ship within 24 to 48 hours. For bespoke custom-engineered shell or V-ring commutators, custom tooling and fabrication typical lead times range from 2 to 4 weeks. Emergency breakdown fast-track services are also available for critical Austrian plant outages.
Yes. Beyond commutator assemblies, we manufacture complete slip ring units, copper pack collector assemblies, constant-force brush holders, and industrial carbon brushes (including electrographite EG251 grades) to provide a complete current collection system overhaul.
Our engineering team is ready to analyze your motor specifications, provide drawing verification, and deliver competitive factory-direct pricing for your project in Austria. Guaranteed response within 24 hours.