Engineered for low-noise operation, IP65/IP66 waterproof protection, IE3/IE4 super-premium efficiency, and seamless VFD speed control.
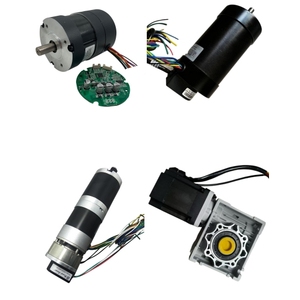
Cooling towers serve as the thermal regulation backbone for petrochemical refineries, power generating plants, commercial HVAC networks, data centers, and heavy processing facilities. Operating continuously in high-humidity, chemically aggressive, and thermally dynamic micro-environments, the motor driving the cooling tower fan is exposed to extreme physical stress. In wet-deck counterflow and crossflow evaporative heat rejection systems, moisture-laden air saturated with scale inhibitors, biocide chemicals, and ambient contaminants creates an aggressive atmosphere that rapidly degrades standard industrial electric motors.
Selecting an optimized cooling tower motor is not merely a matter of horsepower matching; it requires a deep engineering analysis of thermal dissipation coefficients, mechanical shaft sealing, aerodynamic blade load harmonics, and variable torque requirements under shifting atmospheric wet-bulb temperatures. As a premier **China wholesale cooling tower motors manufacturer and factory**, our engineering philosophy centers on delivering **Information Gain** through advanced direct-drive permanent magnet synchronous motor (PMSM) designs, EC/BLDC intelligence, and heavy-duty AC induction motors built to withstand 100% relative humidity (RH) condensing environments.
Historically, large cooling tower applications relied on standard 4-pole or 6-pole AC induction motors connected to right-angle speed reducers (gearboxes) or drive belts to achieve the low fan speeds (typically 150 RPM to 450 RPM) required for optimal aerodynamic airflow. However, these mechanical transmission systems introduce multiple single-point failure modes: gear tooth pitting, oil seal failures, shaft misalignment, belt stretch, and dynamic vibration harmonics that accelerate bearing fatigue.
Modern industrial HVAC procurement strategies favor high-torque direct-drive permanent magnet motors. By pairing a high-pole-count permanent magnet rotor with an integrated sinusoidal Field-Oriented Control (FOC) variable frequency drive (VFD), direct-drive cooling tower motors eliminate the gearbox entirely. This structural evolution yields significant operational improvements:
Direct mechanical coupling transfers 98.5% of electromagnetic shaft torque straight to the fan hub, eliminating gear mesh friction and belt thermal dissipation losses.
Equipped with dual-lip Viton shaft seals, labyrinth oil/slop rings, and vacuum-pressure impregnated (VPI) Class H stator windings to block moisture penetration.
Smooth turndown capabilities down to 10% rated speed allow real-time alignment with thermal wet-bulb fluctuations, maximizing energy savings during off-peak hours.
To assist MEP design consultants, industrial plant operators, and HVAC OEMs in evaluating drive technology choices, the matrix below highlights critical performance parameters across electric motor topologies:
| Performance Indicator | Traditional Belt-Drive Induction | Gearbox-Coupled AC Motor | Direct-Drive EC / PM BLDC Motor |
|---|---|---|---|
| System Energy Efficiency | 78% - 84% (High Belt Friction) | 82% - 87% (Gear Losses) | 92% - 96% (IE4/IE5 Standard) |
| Ingress Protection Rating | IP54 Typical | IP55 Standard | IP65 / IP66 Fully Sealed |
| Acoustic Noise Output | High (Belt Chirp & Sheave Resonance) | Moderate-High (Gear Tooth Mesh) | Ultra-Low (Aerodynamic & Sinusoidal FOC) |
| Annual Maintenance Requirement | High (Belt Tensioning, Alignment) | High (Oil Changes, Seal Check) | Near Zero (Grease-for-life / 100k hr Bearings) |
| Vibration Severity (ISO 10816) | Class II (> 2.8 mm/s) | Class II (> 2.3 mm/s) | Class I (< 0.71 mm/s Precision Balanced) |
| Total Cost of Ownership (5-Yr) | High (Maintenance + Power Loss) | Moderate-High | Lowest (Rapid 14-Month Payback) |
The global industrial cooling tower market is experiencing a structural paradigm shift driven by stringent decarbonization mandates, rising kWh electrical tariffs, and regional environmental standards (such as EU Ecodesign Directive and US DOE Efficiency Standards). Industrial procurement directors must align their supply chain sourcing strategies with four dominant technology trends:
Standard AC induction motors hit a physical threshold where further increases in copper winding volume yield diminishing efficiency gains. Permanent Magnet BLDC motors, utilizing high-coercivity Neodymium-Iron-Boron (NdFeB) magnets, eliminate rotor copper losses completely. China commands over 70% of global rare-earth element processing, giving **China wholesale cooling tower motor factories** a strong structural cost advantage in producing premium PM and EC motor configurations at highly competitive volume pricing.
Unscheduled cooling tower outages can halt production across chemical plants or cause data center server thermal throttling. Next-generation cooling tower motors manufactured in our factory integrate embedded MEMS tri-axial vibration sensors, RTD winding temperature detectors, and moisture-sensing internal probes connected via RS485 Modbus or CANopen protocols. This real-time telemetry allows building management systems (BMS) to predict bearing degradation or moisture ingress long before mechanical failure occurs.
Cooling tower air plumes are saturated with airborne moisture and mineral salts. Modern B2B buyers now specify heavy-duty anti-corrosion surface treatments: C4 to C5-I industrial epoxy paint coatings, 316 stainless steel hardware, and lightweight high-tensile die-cast aluminum alloy frame enclosures (such as our IP54/IP65 compact motor range). These material selections eliminate rust flake accumulation in cooling tower water basins and protect internal laminations from chemical attack.
Rather than purchasing motors, VFD drives, fan impellers, and mounting brackets from disparate suppliers, global OEMs increasingly request factory-assembled, dynamically balanced drive packages. Buying directly from an established manufacturing facility guarantees that electromagnetic resonance frequencies are engineered out of the VFD carrier frequency range, eliminating destructive mechanical harmonics across the speed envelope.
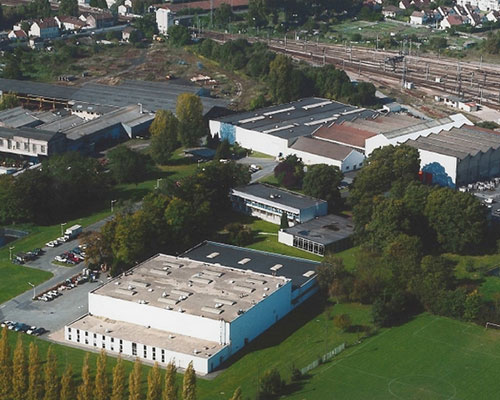
Backed by over a century of industrial rotating machine engineering excellence, our manufacturing facility stands among the premier electric motor producing bases in China. Combining European technical heritage with modern high-volume automated manufacturing, we deliver uncompromised quality control, certified testing protocols, and complete customization capabilities for global enterprise procurement networks.
Every cooling tower motor produced in our factory undergoes rigorous 100% full-load bench testing, high-voltage surge testing, dynamic rotor balancing to ISO 1940 G1.0, and IPX6 waterproof pressure spray testing. Our facility operates under LRQA ISO 9001 certified quality management systems.
As active corporate members of EASA (Electrical Apparatus Service Association) and AEMT (Association of Electrical and Mechanical Trades), our motor designs strictly comply with IEC, NEMA, CE, RoHS, and UL safety standards.
Vibration, thermal rise, dielectric breakdown, and noise spectrum analysis performed on every production batch before dispatch.
Tailored stainless steel extension shafts, special NEMA/IEC flanges, and custom terminal box locations engineered to drop into any cooling tower frame.
Heavy-duty IPPC sea-freight wooden crate packaging with internal VCI vapor corrosion inhibitor bags to guarantee damage-free international arrival.
Elevate your HVAC cooling tower efficiency, reduce maintenance overhead, and secure factory-direct wholesale pricing today. Contact our senior application engineering team for customized motor solutions.