Explore our heavy-duty gearboxes and high-efficiency BLDC/AC drives engineered for continuous S1 industrial duty cycles, extreme shock-load absorption, and high thermal capacity.
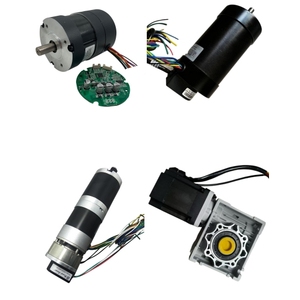
Precision-engineered 3-phase brushless DC geared motor designed for heavy-duty automated positioning. Features integrated dynamic electromagnetic braking and high-resolution encoder feedback.
Get Catalog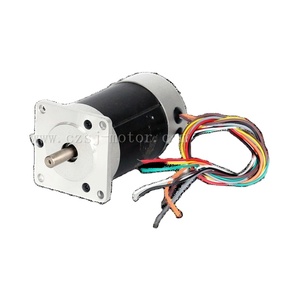
Heavy-duty industrial BLDC motor engineered for demanding variable-speed drive systems. Delivers maximum torque density, minimal thermal losses, and extended bearing lifespan under full loads.
Get Catalog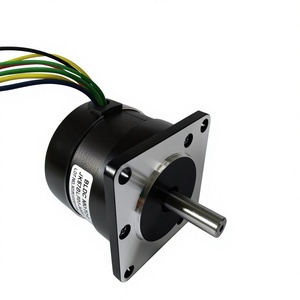
High-speed brushless drive optimized for direct mounting to planetary gearboxes. Built with Class H magnet wire and high-grade neodymium magnets for precise smart control systems.
Get Catalog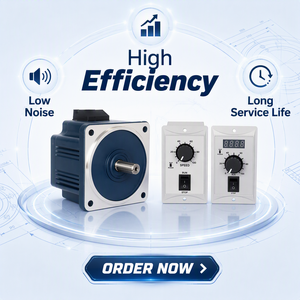
Rugged IP54 waterproof permanent magnet drive designed for hostile industrial environments. Features low acoustic emission, heat dissipation fins, and dynamic rotor balance.
Get Catalog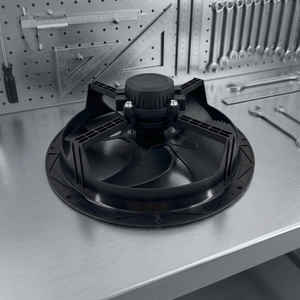
Engineered for cold chain storage, chemical washdown environments, and heavy-duty refrigeration ventilation. Fully epoxy-encapsulated stator prevents condensation buildup.
Get Catalog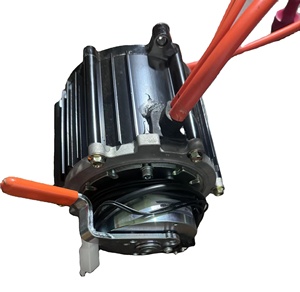
High-load electric traction gear motor designed for industrial utility vehicles and automated guided vehicles (AGVs). Delivers massive starting torque with smooth vector speed control.
Get Catalog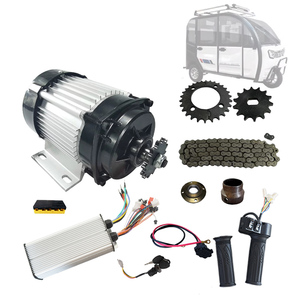
Complete heavy-duty electro-mechanical drive kit featuring reinforced terminal blocks, cast iron mounting flanges, and thermal overload protection for industrial machinery conversions.
Get Catalog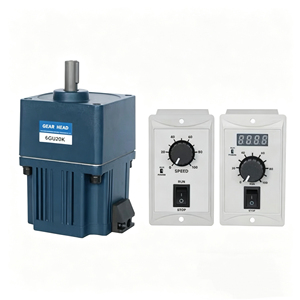
Ultra-quiet aluminum alloy brushless gearhead motor built for space-constrained industrial conveyor lines, medical actuators, and high-precision processing equipment.
Get CatalogIn modern heavy industrial applications—ranging from metallurgy rolling mills and mining conveyors to cement kilns and port handling cranes—the mechanical power transmission assembly represents the primary operational bottleneck. As global industrial procurement strategies evolve beyond initial capital expenditure toward total life-cycle cost optimization, selecting a trusted China heavy duty gearboxes factory & exporter has become a strategic imperative for OEM machine builders and plant asset managers.
China's heavy industrial gear transmission sector has undergone a massive technological shift over the past decade. By pairing advanced metallurgy with computer-controlled carburizing heat treatment and high-precision CNC gear grinding equipment (utilizing Swiss Reishauer and German Gleason gear grinders), top-tier Chinese manufacturers now deliver gear reducers that meet or exceed international standards such as AGMA (American Gear Manufacturers Association), DIN 3962, and ISO 6336.
When evaluating heavy-duty gearboxes, structural integrity, thermal dissipation capacity, and tooth contact stress geometry are the three pillars of operational longevity. Modern gear reducers must withstand extreme torsional shock loads (often reaching 250% to 300% of nominal rating) while maintaining low thermal friction losses to prevent lubricating oil breakdown.
Heavy-duty gear shafts and pinions are forged from high-purity alloy steels such as 20CrMnTi, 17CrNiMo6, or 18CrNiMo7-6. Carburizing and quenching processes achieve a tooth surface hardness of 58-62 HRC while maintaining a ductile, shock-resistant core (33-40 HRC), preventing brittle tooth root fractures under high impact loads.
Using 3D Finite Element Analysis (FEA) and profile tip relief (micro-geometry modification), gear teeth are modified along the flank to compensate for shaft deflection under full torque. This ensures uniform tooth contact pressure across the entire face width, dramatically cutting noise levels below 75 dB(A).
Excessive thermal rise is the leading cause of premature synthetic gear lubricant degradation and lip seal failure. Modern heavy-duty gearboxes incorporate high-surface-area nodular cast iron housing designs (QT450-10), integrated cooling coils, and forced-lubrication oil pumps to maintain sump temperatures below 85°C.
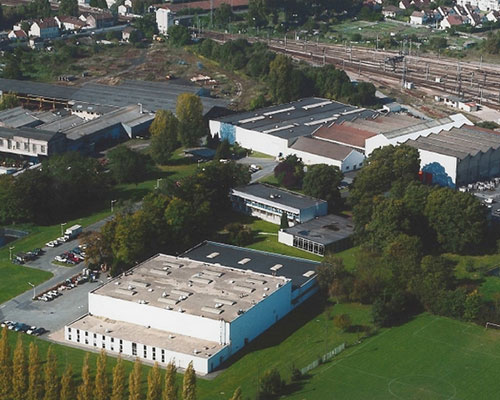
Combining over 120 years of European mechanical engineering heritage through our strategic integration with T-T Electric frameworks, our manufacturing operations deliver world-class rotating machines, industrial DC motors, variable-speed AC drives, and heavy gear transmission systems.
Every gear unit and industrial motor undergoes rigorous non-destructive testing (NDT), magnetic particle inspection for sub-surface micro-cracks, and dynamic 100% full-load bench testing before export packaging. Our facilities are backed by premier international quality credentials:
As global supply chains adapt to environmental directives and Industry 4.0 automation, B2B procurement managers must align their purchasing strategies with upcoming market developments. Key shifts shaping the future heavy-duty gearbox market between 2025 and 2030 include:
Traditional periodic maintenance schedules are rapidly being replaced by real-time condition monitoring. Modern heavy-duty gearboxes are now specified with pre-drilled sensor ports for wireless vibration accelerometers, oil viscosity sensors, and thermal RTD probes. These sensors interface directly with PLC/SCADA systems via IO-Link or Modbus TCP, allowing plant engineers to predict bearing spalling and gear wear weeks before catastrophic failure occurs.
Energy costs represent up to 90% of an industrial drive unit's total life-cycle expense. Sourcing trends show a sharp migration toward direct-coupled gearboxes paired with Permanent Magnet AC (PMAC) or Brushless DC (BLDC) motors meeting IE4 and IE5 efficiency standards. Eliminating belt drives and worm gears in favor of high-efficiency helical and bevel-helical gear trains delivers electrical power savings of 12% to 28% across processing lines.
Global buyers are moving away from proprietary, single-source gearbox designs that create costly downtime risks. Sourcing leads prefer modular gear series (such as H/B industrial gear units) featuring standardized shaft dimensions, interchangeable mounting flanges, and universal foot/flange configurations. This modular approach allows Chinese exporters to assemble custom torque ratios and output shaft variants within 7 to 14 working days.
With stricter environmental regulations around oil disposal, gearbox manufacturing now heavily favors synthetic Polyalphaolefin (PAO) and Polyglycol (PAG) gear lubricants. Synthetic oils double fluid change intervals from 5,000 operational hours to over 10,000 hours, significantly reducing maintenance downtime and carbon footprint.
To aid mechanical engineers and procurement teams in matching drive topologies to their operational needs, the matrix below outlines performance parameters across key heavy-duty gearbox categories:
| Gearbox Type | Efficiency (%) | Torque Range (Nm) | Gear Ratio Range | Backlash (Arcmin) | Primary Industrial Applications |
|---|---|---|---|---|---|
| Heavy Helical Gear Reducer (H Series) | 96% - 98% | 2,000 - 900,000 | 1.25 : 1 to 450 : 1 | < 6 - 10 | Rolling Mills, Mining Conveyors, Heavy Extruders |
| Bevel-Helical Gear Reducer (B Series) | 94% - 96% | 3,000 - 470,000 | 5.00 : 1 to 400 : 1 | < 8 - 12 | Bucket Elevators, Ball Mills, Mixers, Agitators |
| Heavy Planetary Gear Reducer (P Series) | 95% - 97% | 22,000 - 2,600,000 | 25 : 1 to 4,000 : 1 | < 3 - 5 | Port Cranes, Winches, Rotary Kilns, Tunnel Boring |
| Compact Parallel Shaft Gear Motor | 95% - 97% | 200 - 18,000 | 3.77 : 1 to 280 : 1 | < 8 - 14 | Packaging Machinery, Automated Warehouses, AGVs |
Addressing critical technical, operational, and commercial questions commonly raised during international procurement evaluating China's leading heavy-duty gearbox exporters.
Download our complete engineering catalog, request custom ratio calculations, or consult directly with our senior mechanical drive application specialists today.