Explore our premium selection of industrial-grade brushless DC motors, high-torque servo packages, and intelligent control drives built to withstand demanding operational environments.
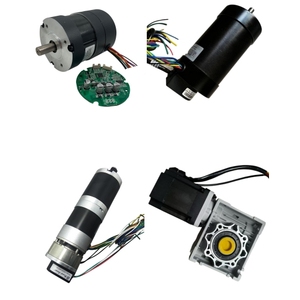
Precision heavy-duty brushless drive solution featuring dynamic electromagnetic braking, high-resolution optical encoder feedback, and wide voltage compatibility (12V to 220V).
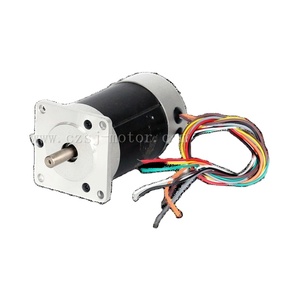
Ultra-high efficiency brushless servo drive power package designed for industrial automation, featuring multi-stage power scalability up to 3000W with exceptional thermal dissipation.
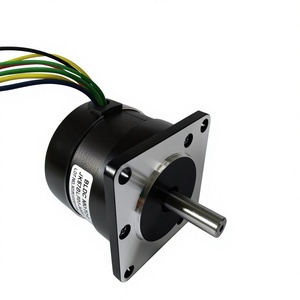
Compact NEMA 23 frame precision drive offering 4000 RPM continuous velocity and 0.22Nm dynamic torque. Ideal for automated smart home systems and medical equipment positioning.
Industrial permanent magnet brushless motor engineered with aluminum alloy heat-sink fins, IP54 weather protection, and ultra-low acoustics for continuous heavy-duty duty cycles.
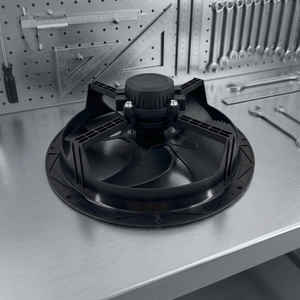
Fully sealed IP65 waterproof permanent magnet motor designed for cold-chain refrigeration, chemical washdowns, and high-humidity HVAC continuous operation.
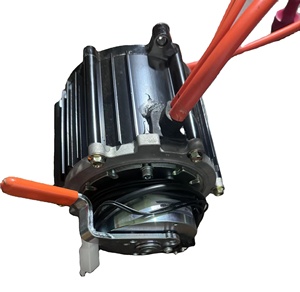
Heavy-duty high-torque brushless drive motor optimized for heavy traction loads, electric vehicle conversion, and high-duty cycle material handling equipment.
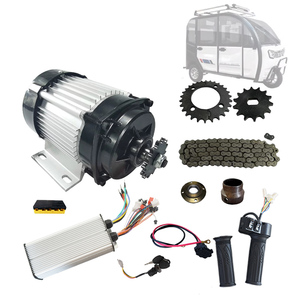
Complete heavy-duty conversion kit combining a 48V 1000W square-wave brushless motor with matched servo controller logic for machinery, karts, and custom industrial rigs.
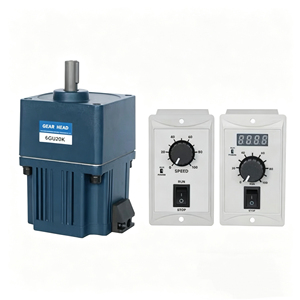
Space-saving, fully enclosed aluminum alloy motor delivering high rotational torque at speeds up to 3000 RPM. Designed for severe dust and splash environment exposure.
An in-depth technical examination of vector control algorithms, power electronics thermal management, and industrial fieldbus integration in modern heavy-duty motion applications.
In modern industrial automation, the demand for dynamic motion control has expanded beyond traditional lightweight robotics into harsh, high-load industrial environments. Selecting the right partner among China best heavy duty servo drives manufacturers & manufacturer networks requires a thorough understanding of electrical power density, field-oriented control (FOC) topology, and thermal dissipation resilience. Modern industrial heavy-duty servo drives serve as the operational nerve center in steel rolling mills, CNC gantry machining, high-speed packaging lines, and heavy-duty electric vehicle conversions.
A heavy-duty servo drive is an advanced power conversion apparatus that dynamically adjusts voltage, frequency, and current phase supplied to a permanent magnet synchronous motor (PMSM) or brushless DC motor (BLDC). Unlike light-duty commercial drives, industrial heavy-duty units are engineered with high thermal capacitance IGBT modules, capable of handling 200% to 300% instantaneous torque overloads while maintaining sub-millisecond position loop responses under extreme vibration and electrical interference.
The core architectural advantage of top-tier industrial servo drives lies in their mathematical field-oriented control algorithms. By decoupling stator current into magnetizing flux ($i_d$) and torque-producing ($i_q$) vector components, the drive maintains maximum torque per ampere (MTPA) across varying velocity regimes. Premium drive manufacturers in China utilize 32-bit floating-point digital signal processors (DSPs) paired with FPGA co-processors to execute current feedback loops in less than 62.5 microseconds.
Silicon Carbide (SiC) and optimized IGBT topologies permit carrier switching frequencies up to 16 kHz, minimizing motor acoustic noise and copper harmonic losses.
Heavy deceleration cycles convert mechanical kinetic energy back into electrical energy. Integrated braking transistors and bus capacitors absorb peak transient voltages without fault tripping.
Universal encoder interfaces support incremental ABZ encoders, absolute BiSS-C, EnDat 2.2 protocols, and rugged electromagnetic resolvers for hot, high-vibration plants.
Thermal management dictates the operational life of heavy-duty drives. Continuous operation at high ambient temperatures can induce power module gate degradation. Leading Chinese servo drive manufacturers implement direct copper bonding (DCB) ceramic substrates, cold-forged aluminum heatsinks, and forced air or liquid cooling channels. Enclosures rated from IP54 to IP65 ensure protection against metallic dust, cutting fluids, and chemical atmospheric pollutants.
The following data matrix outlines critical technical metrics when evaluating heavy-duty servo drives across standard, industrial, and heavy-duty tiers:
| Performance Parameter | Standard Commercial Drive | Industrial Grade Drive | Heavy-Duty Industrial Drive (Our Specification) |
|---|---|---|---|
| Overload Capacity | 120% for 60 seconds | 150% for 60 seconds | 200% - 300% for 3 to 5 seconds |
| Current Loop Bandwidth | 500 Hz | 1.2 kHz | 2.5 kHz - 3.0 kHz |
| Ingress Protection | IP20 (Open Frame) | IP40 / IP52 | IP54 / IP65 Fully Enclosed |
| Vibration Resistance | 1G (10-50 Hz) | 2.5G (10-150 Hz) | 5G - 10G Continuous (IEC 60068-2-6) |
| Fieldbus Protocols | Modbus RTU / RS485 | CANopen / Profibus | EtherCAT (100Mbps), PROFINET RT/IRT, CANopen |
| Operating Temp Range | 0°C to +40°C | -10°C to +50°C | -20°C to +65°C Heavy Duty Ambient |
Understanding key industry shifts empowers procurement managers and system integrators to future-proof their machinery investments.
Modern procurement standards require servo drives to act as edge-computing telemetry nodes. Integrated microcontrollers collect real-time data regarding motor coil temperature, vibration FFT profiles, voltage sag frequency, and total operating hours. Drives communicate wirelessly or through industrial Ethernet to cloud-based predictive maintenance systems, preventing catastrophic line shutdowns.
The transition from silicon-based insulated gate bipolar transistors (IGBTs) to Silicon Carbide (SiC) power MOSFETs is revolutionizing drive energy efficiency. SiC technology enables ultra-fast switching speeds with up to 70% reduction in internal thermal dissipation, yielding smaller drive footprints and higher power density per cubic centimeter.
Industrial machinery builders are shifting away from large centralized control cabinets toward decentralized motor-mounted drives. IP65-rated drive units installed directly on the motor frame reduce expensive shielded motor cabling, diminish electromagnetic emissions, and streamline factory space utilization.
Global safety standards require integrated Safe Torque Off (STO), Safe Stop 1 (SS1), and Safely-Limited Speed (SLS) functional safety features certified to SIL3 / PLe standards. Modern buyers prioritize drive manufacturers who integrate hardware-level safety channels directly onto the drive logic board.
With an engineering legacy spanning over 120 years in electric motor and heavy-duty drive manufacturing, our enterprise combines historical precision craftsmanship with cutting-edge automated production lines.
Every servo drive and motor package undergoes 100% full-load thermal burn-in, insulation impulse testing, and high-voltage dielectric validation prior to dispatch.
As active members of the Electrical Apparatus Service Association and AEMT, our technical designs adhere to global mechanical and electrical engineering standards.
Our dedicated application engineering team delivers complete technical consulting, drive tuning, and field service response within 24 working hours worldwide.
Tailored motor shaft dimensions, custom voltage windings (12V to 690V), and specialized drive control firmware engineered specifically for unique machine builder requirements.
Essential technical answers for electrical engineers, machinery designers, and industrial purchasing directors.
Speak directly with our senior application engineers to receive custom technical drawings, torque-speed curves, and competitive direct factory pricing for your project.