Premium CE Certified Speed Reducers & Integrated High-Efficiency BLDC Drive Units
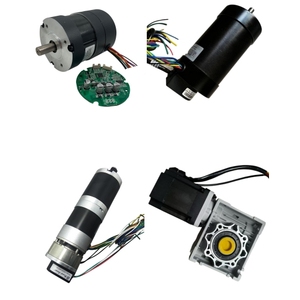
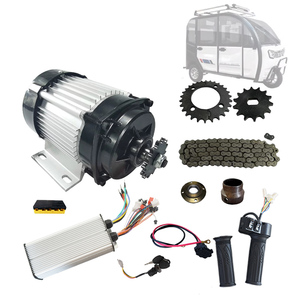
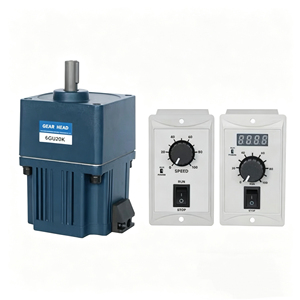
In high-load mechanical transmission systems, the selection of right-angle mechanical reducers represents a critical engineering decision impactive of mechanical conversion efficiency, structural vibration profiles, thermal dissipation limits, and total lifecycle operational expenditure (OPEX). As a premier global manufacturer and certified supplier of CE Certified Worm Gear Reducers, our engineering division integrates over 120 years of precision electromechanical design experience with European quality benchmarks to address the rigorous demands of modern industrial automation.
Key Takeaway for OEM Procurement Directors: CE certification under the EU Machinery Directive 2006/42/EC and Low Voltage Directive 2014/35/EU mandates stringent proof of structural fatigue limits, thermal noise safety, and zero-leakage lubricant sealing integrity under continuous S1 duty cycles.
The core mechanism of a worm gearbox revolves around a non-intersecting, perpendicular shaft arrangement where a hardened steel worm screw meshes with a high-tensile bronze alloy worm wheel (CuSn12 nickel-bronze composite). The unique reduction ratio ($i = z_2 / z_1$) allows high input speeds (ranging from 900 RPM to 3600 RPM) to be converted into ultra-high output shaft torque within a compact physical footprint.
Advanced CAD/CAM tooth-profiling ensures optimized contact line distribution across the gear teeth. By utilizing double-enveloping worm gearing geometry, contact surface area is quadrupled compared to conventional cylindrical worm gearboxes. This dramatically reduces localized tooth bending stress, prevents premature pitting, and improves mechanical efficiency by up to 14% over standard single-enveloping designs.
A inherent characteristic of sliding contact in worm gearing is friction-generated thermal energy. Under continuous heavy duty operational conditions, lubricant breakdown poses the primary threat to gearbox longevity. Our CE-certified reducers incorporate high-conductivity die-cast aluminum alloy housings (sizes 025 to 090) and high-rigidity FC-25 gray cast iron enclosures (sizes 110 to 150).
Engineered cooling fins, combined with synthetic polyglycol (PAG) lubricants pre-filled at the factory, enable continuous operating thermal thresholds up to +95°C without viscosity thermal decay. This design prevents thermal expansion binding and maintains oil-seal integrity (using high-temperature Viton radial shaft seals) over 20,000 continuous operating hours.
Comparative Engineering Data for Plant Engineers & OEM Machine Designers
| Drivetrain Technology | Kinematic Efficiency ($\eta$) | Backlash Range (Arcmin) | Self-Locking Capability | Acoustic Rating (dB) | CAPEX Ratio |
|---|---|---|---|---|---|
| CE Certified Worm Reducer | 65% - 92% (Ratio Dependent) | 10 - 20 | High (Static & Dynamic) | < 58 dB(A) | 1.0 (Optimal Baseline) |
| Helical-Bevel Gearbox | 94% - 97% | 6 - 12 | None (Requires Brake) | 68 - 74 dB(A) | 2.4x Baseline |
| Precision Planetary Reducer | 95% - 98% | 1 - 3 | None | 65 - 70 dB(A) | 3.2x Baseline |
| Cycloidal Speed Reducer | 88% - 93% | < 1 | Conditional | 62 - 66 dB(A) | 2.8x Baseline |
T-T Electric stands as an internationally renowned manufacturer of industrial motor drives and mechanical speed reducers. Established over a century ago, our engineering facility combines European precision tooling with rigorous quality management protocols certified by LRQA (Lloyd's Register Quality Assurance).
As active corporate members of the Electrical Apparatus Service Association (EASA) and the Association of Electrical and Mechanical Trades (AEMT), every CE-certified worm gear reducer and paired BLDC motor undergoes 100% full-load dynamic testing, laser alignment verification, and acoustic spectral analysis prior to dispatch.
Navigating the Shift in Industrial Power Transmission (2025–2030 Roadmap)
Traditional AC induction motors coupled to heavy gearboxes are rapidly being replaced by high-torque permanent magnet Brushless DC (BLDC) motors paired with low-ratio worm gearboxes. This hybrid architecture lowers overall energy consumption by up to 28% while providing precision variable speed control across 1:100 speed ranges.
Modern industrial procurement specifications increasingly demand integrated condition monitoring. Future-ready worm gear units are pre-drilled for vibration sensors (accelerometers) and oil temperature transducers, feeding real-time health data directly into factory SCADA systems to prevent catastrophic mechanical failure.
With global sustainability mandates tighter than ever, procurement teams prioritize manufacturers utilizing 100% recyclable aluminum housings, lead-free synthetic lubricants, and compliance with EU RoHS and REACH directives alongside core CE certifications.
Expert Answers to Critical Engineering and Sourcing Questions
A CE certified worm gear reducer complies with the EU Machinery Directive 2006/42/EC regarding mechanical risk protection and structural integrity, and Directive 2014/35/EU (Low Voltage) when supplied as an integrated gearmotor assembly. Full technical documentation (Technical File) and Declaration of Conformity are provided.
Self-locking occurs when the lead angle of the worm thread is smaller than the static friction angle of the meshing materials (typically when reduction ratios exceed 30:1 or 40:1). This prevents back-driving from the output shaft, serving as a critical safety mechanism in hoisting, elevating, and inclined conveyor systems.
Yes. Our reducers feature standardized IEC and NEMA input flanges (e.g., NEMA 23, IEC 56B14, 63B5, 71B5) with precision keyway and hollow shaft couplings, ensuring seamless integration with 12V, 24V, 48V, and 220V BLDC motors across power ratings from 20W to 3000W.
For synthetic PAG-lubricated aluminum units, oil change is not required under normal operating ambient conditions (-20°C to +40°C) for up to 15,000 continuous hours. For heavy-duty cast iron reducers with mineral oil, initial change is required after 300 operating hours, followed by changes every 4,000 service hours.
Overhung load represents radial force acting on the output shaft. It is calculated using: $F_{rn} = (2000 \times M_2 \times K_k) / d$, where $M_2$ is output torque (Nm), $K_k$ is transmission element factor (e.g., 1.0 for sprockets, 1.25 for gears), and $d$ is pitch diameter. Our engineering catalog lists maximum allowable radial values for all frame sizes.
We provide comprehensive OEM customization including custom output shaft dimensions (single/double solid shafts or spline bores), custom mounting flanges, food-grade synthetic lubricants, IP65/IP66 stainless steel shafts, and specialized corrosion-resistant surface coatings for marine environments.
Request our complete 2025 CE Certified Worm Gear Reducer & Integrated BLDC Motor Catalog or consult directly with our senior mechanical application engineers today.
Get Catalog